

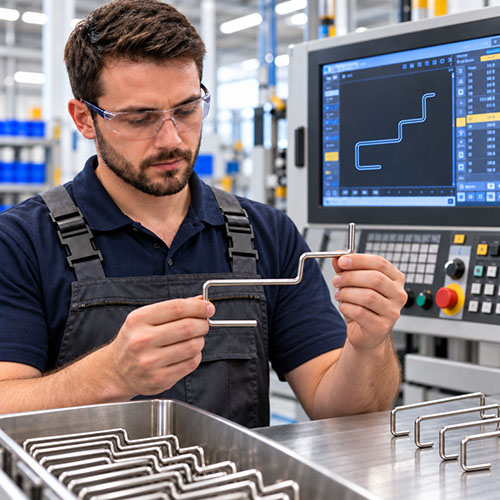
CNC wire forming gives engineers and manufacturers the ability to turn straight or coiled wire into precise two-dimensional and three-dimensional components for automotive, aerospace, material handling, medical, food processing, and general industrial applications. Modern CNC wire bending equipment can produce complex geometries efficiently, but the quality and manufacturability of the finished part still depend heavily on decisions made during the design stage.
Wire diameter, bend radius, tolerances, material selection, bend sequence, and overall geometry all influence how easily a wire form can be manufactured and how consistently it can be reproduced. Designing these features with the forming process in mind can reduce unnecessary complexity, simplify production, and improve repeatability.
This CNC wire forming design guide covers several of the most important factors engineers should consider when developing a custom wire component, from selecting an appropriate wire diameter to establishing realistic dimensional tolerances.
Understanding CNC Wire Forming
CNC wire forming uses computer-controlled equipment to feed, rotate, bend, and cut wire according to a programmed sequence. Instead of manually positioning the material for every bend, the machine controls each movement so that the same geometry can be repeated throughout the production run.
This makes CNC technology especially useful for components containing numerous bends, multiple planes, offsets, loops, or other complex features. A properly designed wire form can often be produced directly from coil with relatively little secondary handling.
Manufacturers requiring production-ready components can use custom CNC wire forming services to produce both relatively simple forms and more complicated three-dimensional wire products.
Wire Diameter Is One of the First Design Decisions
Wire diameter affects nearly every aspect of a formed component. It influences strength, rigidity, weight, bendability, tooling requirements, and the amount of space required to create a particular geometry.
Choosing the largest possible wire diameter does not automatically result in the best design. A thicker wire may provide additional strength, but it can also increase material cost, part weight, bend forces, and minimum practical bend dimensions. Conversely, wire that is too small may not provide enough rigidity or load-carrying capability for the intended application.
The correct diameter should be selected according to what the finished component needs to do.
Consider the Expected Load
Structural requirements should be evaluated before determining wire size. A lightweight retaining clip experiences very different forces than a support frame, basket divider, handle, or material handling component.
Designers should consider whether the wire will primarily experience tension, compression, bending, vibration, impact, or repeated loading. The way force is applied can be just as important as the total amount of force.
Evaluate Required Rigidity
Some wire forms need to flex intentionally, while others must remain relatively rigid. Increasing wire diameter generally increases stiffness, but material selection and component geometry also influence the final behavior.
Adding bends, cross supports, welded connections, or other structural features can sometimes provide the needed rigidity without simply increasing the diameter of every wire in the assembly.
Account for Available Space
Wire forms are frequently installed inside larger assemblies. The diameter must therefore fit within the available clearance while still providing adequate strength.
This is particularly important for components that pass through holes, interface with slots, fit around another part, or operate near moving equipment. A wire form that performs well structurally is still unsuccessful if it interferes with surrounding components.
How Wire Diameter Affects CNC Bending
Wire diameter also affects the forming process itself. As diameter increases, more force is generally required to create a bend. Tooling, machine capability, bend geometry, and material properties must all be considered together.
Larger-diameter wire can also limit how tightly a bend can be formed. Attempting to force an unnecessarily small radius into heavy wire may increase stress in the material and make dimensional consistency more difficult.
For that reason, wire diameter should not be selected independently from the bend radii and overall geometry of the component.
Understanding Bend Radius in Wire Forming
Bend radius describes the curvature created when wire changes direction. It is a fundamental design characteristic because bending does not create a perfectly sharp corner. The material must transition through a radius.
The appropriate bend radius depends on several factors, including wire diameter, material type, material condition, tooling, and the angle of the bend.
Whenever possible, designers should avoid specifying extremely tight bends unless they are necessary for the function of the component. Allowing a practical bend radius can make the part easier to manufacture and can improve consistency from one component to the next.
Why Extremely Tight Bends Can Be Problematic
When wire is bent, material on the outside of the bend stretches while material on the inside is compressed. The tighter the radius, the more concentrated those forces become.
An excessively tight bend can lead to several potential problems. The wire may flatten or distort at the bend, surface damage may occur, or dimensional variation may become more difficult to control. The exact limitations vary considerably depending on the wire material and diameter.
Rather than assuming that a particular radius can be formed, designers should discuss critical bend requirements with the manufacturer early in the development process.
Inside Radius vs. Centerline Radius
Engineering drawings should clearly indicate how a bend radius is being measured. Some dimensions reference the inside surface of the bend, while others may reference the wire centerline.
Ambiguity can create unnecessary problems during quoting, programming, and inspection. Clearly defining the dimensioning method makes it easier for the manufacturer and customer to evaluate the same feature consistently.
Springback and Its Effect on Wire Form Geometry
Metal does not always remain at the exact angle to which it is initially bent. After forming pressure is removed, the material can recover slightly toward its original position. This behavior is known as springback.
The amount of springback depends on material properties, wire diameter, bend radius, bend angle, and other factors. Stainless steel, carbon steel, and other wire materials can behave differently during forming.
CNC programming and tooling can compensate for predictable springback by bending the material beyond the final desired position. However, the component still needs to be designed within practical forming limits.
Prototype development can be particularly useful when a part contains multiple critical bends or when several bends interact with one another.
Establishing Practical Tolerances for CNC Wire Forms
Tolerances define the acceptable amount of dimensional variation in a manufactured component. Proper tolerancing is essential, but specifying unnecessarily tight tolerances can add complexity without improving the performance of the finished product.
A tolerance should reflect what the component actually needs in order to function properly within the assembly.
Identify Truly Critical Dimensions
Not every dimension on a wire form requires the same degree of precision. Features that locate the component within an assembly, engage another part, or determine overall fit may require closer control.
Other dimensions may have little effect on function and can tolerate greater variation.
Separating critical dimensions from noncritical ones allows the manufacturing process to focus precision where it provides the most value.
Avoid Over-Tolerancing the Drawing
Applying extremely tight tolerances to every bend, length, and angle can make a relatively straightforward wire form unnecessarily difficult to manufacture and inspect.
Tighter tolerances may require additional process development, inspection, fixtures, secondary operations, or production controls. If those requirements do not improve the performance of the component, they can add cost without providing a meaningful benefit.
Designers should therefore ask whether a tolerance is functionally necessary rather than simply applying the smallest possible value.
Tolerance Stack-Up in Multi-Bend Wire Forms
Complex wire forms may contain numerous bends positioned relative to one another. Small variations at individual bends can accumulate across the component, creating what is commonly known as tolerance stack-up.
For example, a three-dimensional wire frame containing several sequential bends may meet individual bend requirements while still showing measurable variation at the final endpoint. The longer and more complex the bend sequence becomes, the more important it is to identify which final dimensions are actually critical.
Dimensioning directly from important functional features rather than relying entirely on a chain of incremental dimensions can make a drawing easier to manufacture and inspect.
Bend Angle and Bend Sequence Matter
A CNC wire forming machine does more than create individual bends. It follows a sequence in which the wire is fed, rotated, and bent repeatedly until the final geometry is produced.
The order of those bends matters because previously formed sections of the component must remain clear of the machine tooling as subsequent features are created.
A wire form that appears straightforward in a CAD model may become difficult to manufacture if one bend prevents access to another. Complex shapes may require modifications to bend sequence, geometry, or tooling to avoid interference.
Early design review can help identify these issues before the component reaches full production.
Designing Three-Dimensional Wire Forms
One of the major advantages of CNC wire forming is the ability to produce bends across multiple planes. Rather than being limited to a flat two-dimensional shape, the wire can be rotated between bends to create complex three-dimensional geometries.
These capabilities are useful for brackets, frames, handles, retainers, supports, baskets, fixtures, and numerous custom components.
However, three-dimensional designs introduce additional considerations. Designers need to account for clearance between sections of wire, orientation of adjacent bends, overall envelope dimensions, and how the finished part will be inspected.
A model or detailed drawing that clearly communicates the intended geometry is particularly valuable for complicated 3D wire forms.
Material Selection Affects Formability
Different metals behave differently during bending. Strength, hardness, ductility, and surface condition can all influence how readily a wire can be formed and how much springback occurs.
Carbon steel and stainless steel are commonly used for industrial wire components, but the correct material depends on the application. Stainless steel may be preferred where corrosion resistance or cleanliness is important, while carbon steel can provide a strong and economical foundation for components that may receive a secondary coating or finish.
The grade and condition of the material should also be considered. Two wires with the same nominal diameter can behave differently during forming if their material properties differ significantly.
Allow Enough Clearance Between Wire Features
Closely spaced features can create manufacturing challenges, particularly when several bends, loops, or parallel sections are positioned near one another.
Adequate clearance may be required for forming tools to access the wire without contacting previously formed sections. Clearance can also simplify welding, coating, inspection, and assembly.
If a component contains extremely tight spacing, it is helpful to identify which clearances are functionally required and which can be adjusted to improve manufacturability.
Consider Secondary Operations During the Design Stage
Wire forming is often one step within a larger fabrication process. The formed component may later be welded, attached to a frame, coated, plated, electropolished, or incorporated into another assembly.
Those downstream operations should be considered when developing the initial geometry.
For example, a wire form that will be welded into a basket may need consistent locating points so it can be positioned accurately within a fixture. A component that will receive a coating may require allowances where coating thickness could affect fit. A stainless steel component intended for demanding cleaning environments may require a finish appropriate for that process.
Looking at the entire manufacturing sequence can prevent design changes later in production.
Designing Wire Forms for Welding and Larger Assemblies
Many CNC-formed components eventually become part of larger fabricated products. Wire forms may serve as dividers, handles, reinforcement, product supports, guides, or structural elements within custom wire baskets, carts, racks, and fixtures.
When welding will be required, designers should consider joint access, locating features, contact points, and how the assembly will be fixtured. Simplifying the way components align before welding can improve repeatability and make production more efficient.
The same principle applies to assemblies containing multiple formed-wire components. Designing common reference points and practical connections can simplify both fabrication and inspection.
Use Prototyping to Validate Complex Wire Forms
Prototyping is particularly valuable when a wire form includes unusual geometry, critical interfaces, multiple three-dimensional bends, or an application where fit must be verified against existing equipment.
A prototype allows engineers to evaluate the real component rather than relying entirely on a CAD model. Issues involving clearance, installation, loading, ergonomics, and interaction with surrounding components can often be identified before production quantities are manufactured.
Salco’s design and prototyping capabilities can also help customers refine components before moving into repeat production.
Common CNC Wire Forming Design Mistakes
Many manufacturing challenges can be avoided by considering the forming process earlier in the design cycle. Common issues include specifying a wire diameter without considering bend geometry, requiring unnecessarily tight bend radii, applying restrictive tolerances to noncritical dimensions, creating features with insufficient tooling clearance, and designing a complex bend sequence without considering how the part will be manufactured.
Another common issue is focusing only on the wire form itself rather than its role within the final product. Installation clearances, welding, coatings, loading methods, and the surrounding assembly can all influence whether a design performs successfully.
Design for Function First and Manufacturability Second
Design for manufacturability does not mean compromising the function of the component. Instead, it means achieving the required function without introducing unnecessary manufacturing difficulty.
If two geometries perform equally well but one uses fewer bends, more practical radii, and realistic tolerances, the simpler design may be easier to produce consistently. Similarly, a small dimensional adjustment that provides more tooling clearance can sometimes eliminate an unnecessary secondary operation.
Collaboration between the designer and wire forming manufacturer is often most useful before the drawing is finalized. At that stage, adjustments can usually be made more easily than after tooling, programming, prototypes, and production processes have already been established.
Preparing a CNC Wire Forming Project for Quoting
The more information available at the beginning of a project, the easier it is to evaluate the wire form accurately. Useful information can include a dimensional drawing or 3D model, wire diameter, material specification, critical tolerances, estimated production quantity, surface finish requirements, and an explanation of how the component will be used.
Identifying critical dimensions and functional requirements is especially helpful. A manufacturer can then focus on the features that directly affect fit and performance while reviewing other areas for potential manufacturing improvements.
Better Wire Form Design Starts With the Manufacturing Process
Successful CNC wire forming involves more than programming a series of bends. Wire diameter, bend radius, tolerance, springback, material properties, tooling clearance, bend sequence, and secondary fabrication requirements all influence the finished component.
Considering these factors during the design stage can make a wire form easier to manufacture, improve repeatability, and reduce the likelihood of costly revisions after production begins.
For especially complex components, working with the manufacturer before the design is finalized can also uncover opportunities to simplify geometry, establish more practical tolerances, and ensure that the finished part can be produced efficiently.
Salco Engineering provides CNC wire forming and custom wire bending services for industrial components and fabricated assemblies. Using CNC wire forming technology, Salco can produce custom two-dimensional and three-dimensional wire components for a wide variety of manufacturing applications.
If you have a wire form drawing, prototype, or new component that needs to be evaluated for production, contact Salco Engineering to discuss wire diameter, bend geometry, tolerances, materials, production quantities, and other project requirements.